Blistering is a common surface defect in aluminum extrusion. It appears as localized raised areas or blisters on the surface of the extruded profile.
A blister indicates a subsurface cavity or separation beneath a relatively thin surface layer. However, this does not mean that every blister originates from gas porosity already present in the billet. In conventional 6xxx extrusion, an important cause is air trapped and sealed in the container when the billet is loaded. If the air is not adequately released, it may be incorporated into the billet surface region and subsequently carried into the extrusion flow. Other mechanisms are also possible. In particular, hydrogen-related blistering can occur in some high-strength aluminum alloys.
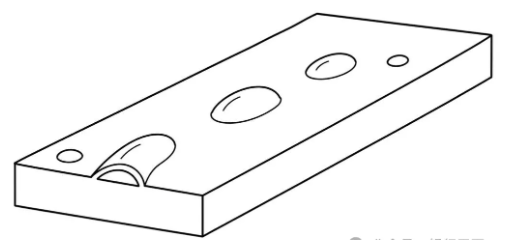
(Typical appearance of blisters on an aluminum extrusion surface)
What does an extrusion blister look like?
A blister is a localized swelling of the profile surface. It may be round or elongated, and its size varies widely.
The blister surface may initially remain intact. If the raised area is broken, cut, or ground, a cavity or separation is often found beneath the surface. Blisters may appear individually or as a series of defects. Some are visible immediately after extrusion, while others become more obvious during subsequent heating as gas in the subsurface cavity expands. The location of blisters along the extrusion can also provide important clues to their origin.
How do trapped-air blisters form?
In direct extrusion, the billet is slightly smaller than the container bore. After loading, it rests at the bottom of the container, leaving air between the billet surface and the container liner. When pressure is applied, the billet shortens and expands until it fills the container. This is called the upsetting process. The billet expansion is not necessarily uniform. As the billet contacts the liner, air pockets may be enclosed. Air pockets may also form near the corner between the container wall and the die face during this upsetting flow.
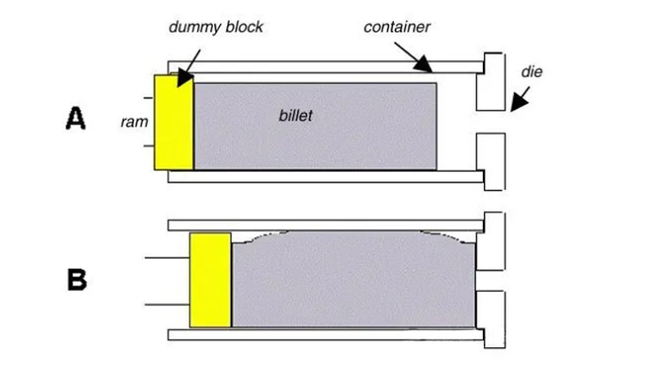
(Before and after upsetting: (A) before extrusion; (B) upsetting.)
The venting cycle is intended to release compressed air before extrusion proceeds. Its timing is important. If decompression occurs too early, contact between the billet and the liner may not yet have formed, and air may remain trapped. If extrusion begins before decompression, trapped air may be incorporated into the billet surface region. Therefore, there is no universal venting pressure suitable for all extrusion conditions.
Effective venting must occur at the correct stage of billet breakthrough.
Where do blisters usually appear? The location where air is trapped in the container does not necessarily correspond to the location where blisters later appear on the extruded part. Trapped air can move along the same flow paths as the billet surface. Material near the container wall moves more slowly because of friction and may later move toward the die as typical back-end flow or coring. Therefore, air trapped during extrusion can eventually cause blistering at the back end of the extrusion. This also explains the importance of adequate venting: extrusion should stop before poor back-end surface material reaches the die.
The cause of front-end blistering may be different. Jowitt, Hay and Parsons reproduced this type of defect when air was trapped in front of a new billet and aluminum remained in the die orifice. They called these transverse weld blisters. Poor container-mouth shear, residual aluminum around the die orifice, or volatile materials such as lubricating oil can also contribute to this mechanism. Therefore, blister location is helpful for troubleshooting. Back-end blistering should prompt attention to air flow and billet surface flow. Front-end blistering should also prompt attention to transverse welds, butt shear, and die condition. These are diagnostic clues, not absolute rules.
Trapped air or hydrogen?
Not all extrusion blisters have the same origin.
In conventional 6xxx extrusion, an important mechanism is air trapped during billet upsetting and subsequently incorporated into the billet surface flow. In high-strength alloys, especially 7xxx alloys such as 7075, hydrogen can provide a different blistering mechanism. Hydrogen may come from the billet itself or be introduced during subsequent processing. During heating or solution heat treatment, hydrogen accumulating in a subsurface cavity can expand and produce visible blisters. For normal 6xxx extrusion, the extrusion cycle should be checked first before assuming that blistering proves the presence of gas porosity in the original billet.
Causes and prevention
Preventing blisters requires control of the entire extrusion cycle, not a single parameter. Important factors include proper billet loading and upsetting, effective venting, clean butt shear, no unnecessary lubricant or other volatile contaminants around the billet/die interface, and sufficient butt discard. The location and timing of defects should always be recorded. Comparing billet batches can also help distinguish press-related problems from billet/container-related problems.
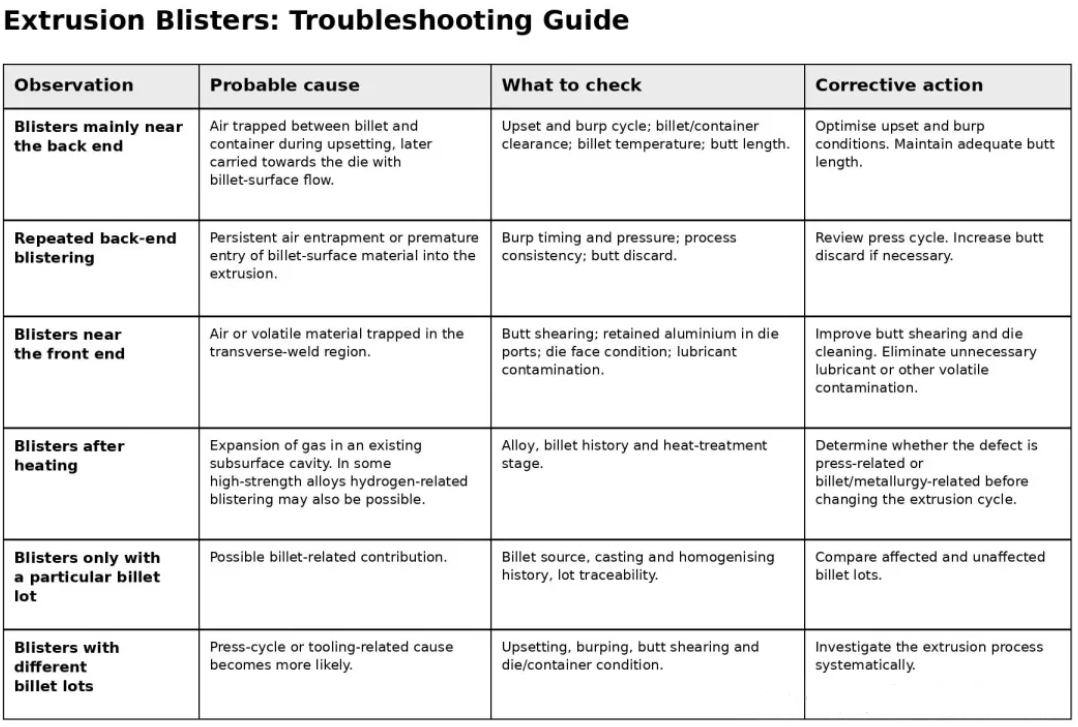
(Aluminum extrusion blister troubleshooting guide: typical observations, possible causes, and corrective actions)
Blisters should also be distinguished from speed cracks in aluminum extrusion, which form by a different mechanism. No universal venting pressure or butt length can prevent blistering on every press stroke. These parameters must be determined for the specific extrusion, billet, alloy, and extrusion conditions. In conventional 6xxx extrusion, an important mechanism is air trapped during billet upsetting and subsequently carried into the extrusion through billet surface flow. Front-end blistering may be associated with the transverse weld zone, while hydrogen-related blistering in high-strength alloys represents a different mechanism. Effective troubleshooting therefore requires identifying where gas was trapped and how the affected material subsequently moved through the extrusion process.
The venting cycle is intended to release compressed air before extrusion proceeds. Its timing is important. If decompression occurs too early, contact between the billet and the liner may not yet have formed, and air may remain trapped. If extrusion begins before decompression, trapped air may be incorporated into the billet surface region. Therefore, there is no universal venting pressure suitable for all extrusion conditions.
Effective venting must occur at the correct stage of billet upset/breakthrough.
Where do blisters usually appear?
The location where air is trapped in the container does not necessarily correspond to the location where blisters later appear on the extruded part. Trapped air can move along the same flow paths as the billet surface. Material near the container wall moves more slowly because of friction and may later move toward the die as typical back-end flow or coring. Therefore, air trapped during extrusion can eventually cause blistering at the back end of the extrusion. This also explains the importance of adequate venting: extrusion should stop before poor back-end surface material reaches the die.
The cause of front-end blistering may be different. Jowitt, Hay and Parsons reproduced this type of defect when air was trapped in front of a new billet and aluminum remained in the die orifice. They called these transverse weld blisters. Poor container-mouth shear, residual aluminum around the die orifice, or volatile materials such as lubricating oil can also contribute to this mechanism. Therefore, blister location is helpful for troubleshooting. Back-end blistering should draw attention to air flow and billet surface flow. Front-end blistering should also prompt attention to transverse welds, butt shear, and die condition. These are diagnostic clues, not absolute rules.
 Aluminum Extrusions
 Fabrication
 Surface Finishes
 Flat Rolled Aluminum